
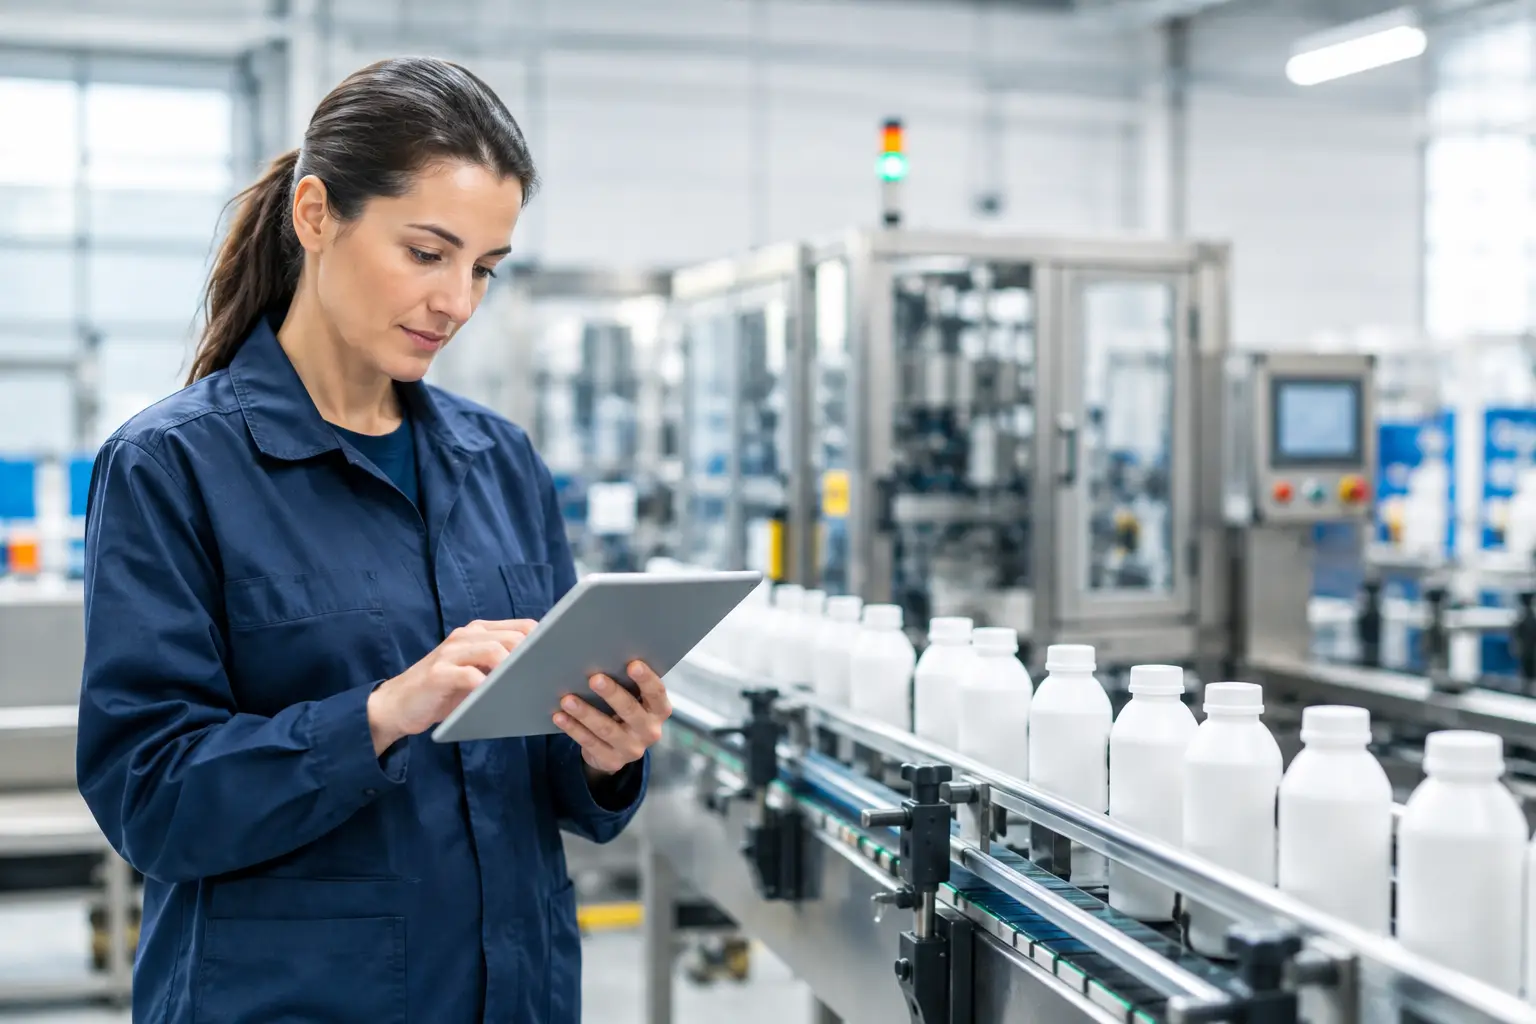
A production line can lose a full shift over a fitting, valve, heater, or fixture that represents a small fraction of the total material cost. That is the central problem in this factory fulfillment case study: keeping a modular-building manufacturer supplied with commercial plumbing materials without flooding its floor, tying up cash in excess inventory, or creating documentation gaps that delay approval.
This is a representative composite scenario based on the fulfillment pressures common to assembly-line and project-based manufacturing. The purpose is not to promise a fixed outcome. Every factory has different bill-of-material accuracy, storage capacity, engineering controls, and supplier lead times. It does show the operating discipline required when material availability directly affects production output.
The Production Problem
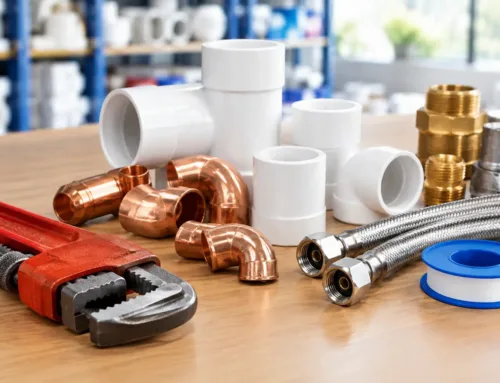
The manufacturer produced modular restroom and utility assemblies for commercial and public-sector projects. Each unit required a repeatable package of copper tubing, valves, drains, water heaters, washroom fixtures, and related components. Some products were standard across several unit types. Others changed by customer specification, accessibility requirements, or approved manufacturer requirements.
The factory’s original purchasing process was workable when output was low. Buyers placed orders against forecasts, received large deliveries, and pulled material from a central storage area. As production volume increased, the weaknesses became more costly. A shortage discovered at a work cell could stop a crew waiting for one approved component. Excess material occupied valuable floor space. Substitute requests created engineering questions, and missing cut sheets or compliance documents slowed release for regulated work.
The issue was not simply inventory quantity. The factory needed the right item, in the right configuration, tied to the right unit schedule, with the required documentation available before the line reached that stage of assembly.
Factory Fulfillment Case Study: Building the Supply Plan
The first step was to separate recurring production material from project-specific exceptions. This distinction matters because these materials should not be managed the same way.
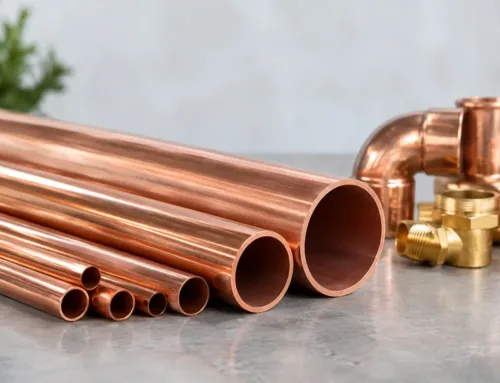
Recurring items included commonly used tubing sizes, fittings, commercial drains, and standard valves. The factory established usage patterns for those components based on planned weekly output, expected scrap, and a practical safety stock level. The goal was not to hold the maximum possible inventory. It was to prevent routine consumption from becoming a daily purchasing emergency.
Project-specific items included selected drinking fountains, bottle-filling coolers, accessible shower components, electric water heaters, and fixtures required by a particular bid package. These products were assigned to a project release schedule rather than treated as general stock. That reduced the chance that an approved component intended for one contract would be consumed on another job.
A fulfillment partner then worked from three basic inputs: the current bill of materials, the production schedule, and the approved-submittal status. When those inputs were current, material could be released in phases aligned with actual assembly needs. When they were not current, the problem could be identified before a shortage reached the floor.
Material was released by production need, not purchase convenience
Large deliveries can look efficient on a freight invoice while creating operational waste inside a factory. In this case, phased releases were used to deliver production-ready quantities to match the next assembly window. The receiving team had enough material to support scheduled work without using staging areas as long-term storage.
Release timing depended on the item. Commodity copper and common fittings could be replenished more frequently. Long-lead equipment required earlier planning and clear confirmation of manufacturer availability. Products with a higher risk of revision were held until the project team confirmed specifications and approvals.
This approach required communication, not just an automated reorder point. If the factory added a shift, changed a unit mix, or moved a customer deadline forward, the supply plan had to change with it.
Documentation moved ahead of material
For public-sector and military construction work, a carton on the dock does not necessarily mean the item is ready for installation. Product data, manufacturer information, submittals, and approval processing can determine whether a component is accepted.
The factory therefore treated documentation as part of fulfillment. For controlled products, the purchase record was tied to the applicable product information and project requirements before the release date. This gave procurement and quality teams time to identify discrepancies before a unit was built around an unapproved item.
That process also reduced a common source of rework: ordering a product that appears equivalent in function but does not match the specified manufacturer, finish, electrical requirement, accessibility detail, or project documentation standard.
What Changed on the Factory Floor
The practical improvement was visibility. Buyers could see which materials supported the next scheduled units, which products were tied to pending approvals, and which items needed an earlier sourcing decision.
Production supervisors gained a more reliable signal on what would be available for the next work cycle. Instead of discovering missing parts during installation, they could flag shortages during planning meetings, when alternatives or expedited sourcing were still possible. That distinction protects labor. A shortage found two weeks ahead is a purchasing task. A shortage found at the work cell is a production disruption.
Receiving also became more organized. Deliveries were identified by project, release, or production need rather than arriving as loosely connected purchase orders. The factory could direct materials to the appropriate staging area and reduce the time spent sorting, searching, and reconciling components after delivery.
For a wholesale partner such as Clarke Plumbing Specialties, the job extended beyond taking an order. It required checking availability, tracking releases, supporting submittal needs, and pursuing hard-to-source material when an approved specification put the schedule at risk.
The Trade-Offs That Required Attention
Phased fulfillment is not a cure for poor planning. It can reduce excess inventory, but it also increases the importance of accurate schedules and prompt communication. If a factory changes its build sequence without notifying suppliers, material may arrive correctly for the old plan and still be late for the new one.
Consolidating spend with one supply partner can simplify accountability and documentation. However, buyers should still evaluate manufacturer lead times, freight exposure, and the risk associated with single-source specified products. A dependable supply plan identifies those constraints early rather than assuming every item can be expedited.
There is also a balance between safety stock and working capital. High-usage, low-cost components may justify a deeper on-site buffer because a shortage can stop multiple assemblies. Expensive equipment, specialized fixtures, and items subject to project revisions generally need tighter release control. The right level depends on consumption rate, replacement lead time, storage conditions, and the cost of a missed production day.
Operating Practices That Made the Difference
The most effective part of the case was not a single product or software tool. It was a repeatable operating rhythm. Production, procurement, engineering, and the supply partner reviewed upcoming work on a set schedule. Open approvals and long-lead items received attention before routine orders. Material changes were documented clearly, with no assumption that a field substitution would be acceptable.
The factory also maintained a short list of critical items: products with long lead times, strict approval requirements, limited manufacturer options, or a direct effect on several assemblies. Those items were monitored separately from standard replenishment material. This focused effort where a missed delivery would have the greatest operational impact.
For procurement teams, the lesson is straightforward. A factory does not need every plumbing item in the building at all times. It needs a controlled flow of approved material that matches what the line will build next. When supply planning, documentation, and responsive sourcing work together, purchasing becomes part of production control rather than a last-minute recovery function.
The next time a line schedule is reviewed, treat the material release plan with the same discipline as labor assignments and equipment availability. The part that stops the line is rarely the most expensive one, but it is always expensive once the crew is waiting.

Leave A Comment